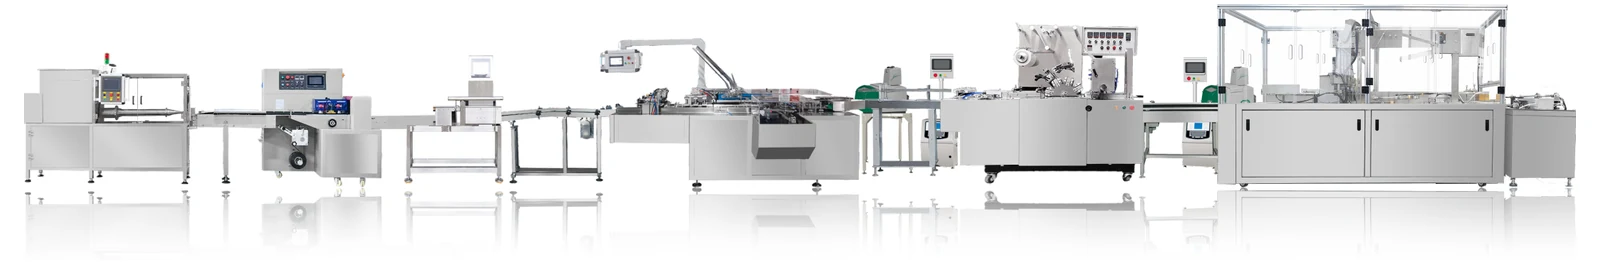
1. End-to-End Shisha Tobacco Packaging Lines
High-volume shisha brands commonly sell 50 g, 100 g, 250 g, or 500 g portions packaged as a sealed inner foil/film pillow block inside a printed folding carton, finished with a clear 3D BOPP/cellophane outer wrap and tear tape (often grouped into 10-box master bundles). Coordinating those steps manually across disconnected machines creates buffer bottlenecks, weight-check gaps, and high labor overhead.
Within the shisha packaging equipment range, an integrated shisha tobacco packaging line links primary dosing and wrapping directly to secondary inspection, cartoning, coding, and 3D cellophane overwrapping. Depending on your workshop floor dimensions and secondary inspection requirements, you can configure either a Straight-Line Hookah Packaging Line (8 numbered stations) or a Corner-Type Hookah Packaging Line (5 numbered stations).
For leaf sorting, cutting, molasses mixing, and bulk hopper transfer ahead of packaging, read our Shisha Processing Machine Guide. If you are comparing wet molasses shisha lines against dry cut-rag or pipe tobacco equipment, review our Tobacco Packing Line Guide for dosing, barrier liner, and cartoning differences.
2. Straight-Line (8-Station) vs Corner-Type (5-Station) Layouts
Compare how the stations are arranged across both turnkey line topologies:
| Line Feature | Straight-Line Hookah Packaging Line (8 Stations) | Corner-Type Hookah Packaging Line (5 Stations) | Factory Planning Impact |
|---|---|---|---|
| Layout geometry | Linear inline arrangement from infeed to bundle discharge | 90-degree L-shaped turn layout | Corner layout fits shorter workshop bays with wider cross-aisles |
| Station 01 | Extruder (sticky shisha metering & block forming) |
Extruder (sticky shisha metering & block forming) |
Sets portion weight consistency feeding the wrapper |
| Station 02 | Pillow packaging machine (e.g. LV-350SY Horizontal Flow) |
Pillow packaging machine |
Seals inner foil/film pillow pack (100–500 g envelope) |
| Station 03 | Checkweigher (primary inner-pack weight check) |
Boxing machine (automatic cartoner after 90° transfer) |
Straight line adds dedicated pre-carton checkweighing |
| Station 04 | Boxing machine (automatic folding-carton inserter & closer) |
Inkjet printer (date, batch, or tax coding on carton) |
Hot-melt glue or tuck-flap carton closure options |
| Station 05 | Weight sorting (secondary filled-carton checkweigher) |
Small-box 3D cellophane overwrapper |
Wraps individual retail cartons in clear BOPP film |
| Station 06 | Inkjet printer (carton date & traceability coding) |
(Optional downstream bundling) | Confirm print height, character lines, and tax-stamp needs |
| Station 07 | Small-box 3D cellophane overwrapper |
— | Individual carton moisture & tamper-evident overwrap |
| Station 08 | Large-box 3D cellophane overwrapper |
— | Collates and overwraps multi-carton master bundles |
3. Single-Box & Multi-Pack 3D Cellophane Overwrapping
After inner pillow packs are inserted into folding cartons and coded, secondary overwrapping protects aroma retention and shelf presentation:
- Individual Carton 3D Overwrapping (
Station 07on Straight-Line /Station 05on Corner-Type): Wraps each folding carton in clear BOPP/cellophane film with precision envelope-folded corners and an integrated tear-off tape strip. - Master Bundle 3D Overwrapping (
Station 08on Straight-Line): Collates multiple wrapped retail boxes (for example, 5 or 10 cartons per bundle) and applies a tight outer 3D film wrap ready for master case packing.
For envelope end-fold mechanics, BOPP sealing temperatures, board stiffness limits, and multi-size mold changeovers between single retail boxes and 5- or 10-box bundles, read our Carton Overwrapping Machine Guide.
4. How Station-to-Station Synergy Protects Profit & Uptime
A standalone LV-350SY Horizontal Flow Wrapper is rated at 50–120 bags/min, but real-world shift profitability depends on how upstream extrusion, weight verification, cartoning, and 3D overwrapping work together:
- Cohesive Extrusion Prevents Cartoner Jams (
Station 01→02→04): When inner bags are over-inflated or unevenly filled, flaps jam inside automatic boxing machines. Pairing01. Extruderwith02. Pillow packaging machineforms a compact, flat-profile100–500 gblock with clean cross seals, ensuring smooth insertion at04. Boxing machine. - Pre-Carton Checkweighing Saves Printed Boxes (
Station 03&05): What you waste, you cannot sell. The 8-station straight-line layout places03. Checkweigherimmediately after the pillow wrapper so underweight or overweight inner bags are rejected before consuming a printed folding carton or BOPP film—followed by05. Weight sortingafter boxing to catch missing-insert or double-pack errors. - Balanced Cartoning & 3D Overwrapping (
Station 04,07,08): Turret 3D cellophane wrappers typically cycle at lower speeds than a high-speed pillow wrapper. Synchronizing conveyor indexing prevents pile-ups between stations. For a step-by-step shift calculation, read our Shisha Packaging Line Capacity Planning Guide.
5. Alternative Line Topologies: Premade Pouches or Rigid Tubs
Not every turnkey line uses a pillow wrapper + cartoner:
- Premade Pouch Line: Pairs a LV-350SY Premade Pouch Packing Machine (
10–20 bags/min) with a discharge checkweigher, metal detector, and rotary accumulation table. - Rigid Tub / Bottle Line: Uses the Hookah Bottle Filling Line (unscrambler → indexing → dosing → screw capping → aluminum foil sealing → round labeling → sorting).
Compare all format options in Shisha Tobacco Packaging Formats and How to Choose a Shisha Packing Machine.
6. Workshop Layout, Utilities & Handover Planning
Because integrated lines span multiple linked conveyors, your RFQ and engineering review must lock down:
- Floor dimensions & column locations: Decide between the linear 8-station straight line and the L-shaped 5-station corner line based on available bay length and forklift aisles.
- Electrical & pneumatic schedule: Consolidate individual station power (e.g.
220V 50/60Hzsingle-phase wrappers vs three-phase cartoners/extruders) and clean, dry compressed air. - Integrated FAT & On-Site Commissioning: Require the complete connected line—not just isolated machines—to run your inner film, folding cartons, and BOPP overwrap film during the Factory Acceptance Test (FAT), and review Installation, Training & After-Sales Support.
7. Frequently Asked Questions
When should I choose the Corner-Type line instead of the Straight-Line layout?
Choose the Corner-Type Hookah Packaging Line (5 stations) when your packaging room lacks the linear length required for an 8-station straight line, or when you only need single-carton 3D cellophane overwrapping without a secondary checkweigher and master-bundle overwrapper.
Can we buy the primary pillow wrapper first and add the cartoner and 3D wrapper later?
Yes. Many plants start with the extruder + LV-350SY Horizontal Flow Wrapper (100–500 g) and manual boxing, then add the automatic cartoner and 3D cellophane overwrapper once daily carton volume justifies full automation. Review staged budgeting in our Shisha Packing Machine Price Guide.
How do you handle flavor changeovers on a full packaging line?
Only the upstream extruder/hopper and primary forming chute contact raw wet shisha molasses; downstream checkweighers, cartoners, coders, and 3D overwrappers handle sealed inner packs. Read Cleaning & Flavor Changeover for upstream washdown procedures.
8. Request a Turnkey Shisha Packaging Line Proposal
Share your inner pack weight, carton dimensions (L × W × H), bundle count, and available floor space with LINEVO directly on WhatsApp.
Configure Your Shisha Packaging Line with LINEVO Engineers
Send your shisha tobacco pack format, target gram weight, and required speed on WhatsApp to receive technical drawings, trial videos, and an itemized factory quotation, or check our RFQ preparation checklist.
Get Quote via WhatsAppBack to equipment overview