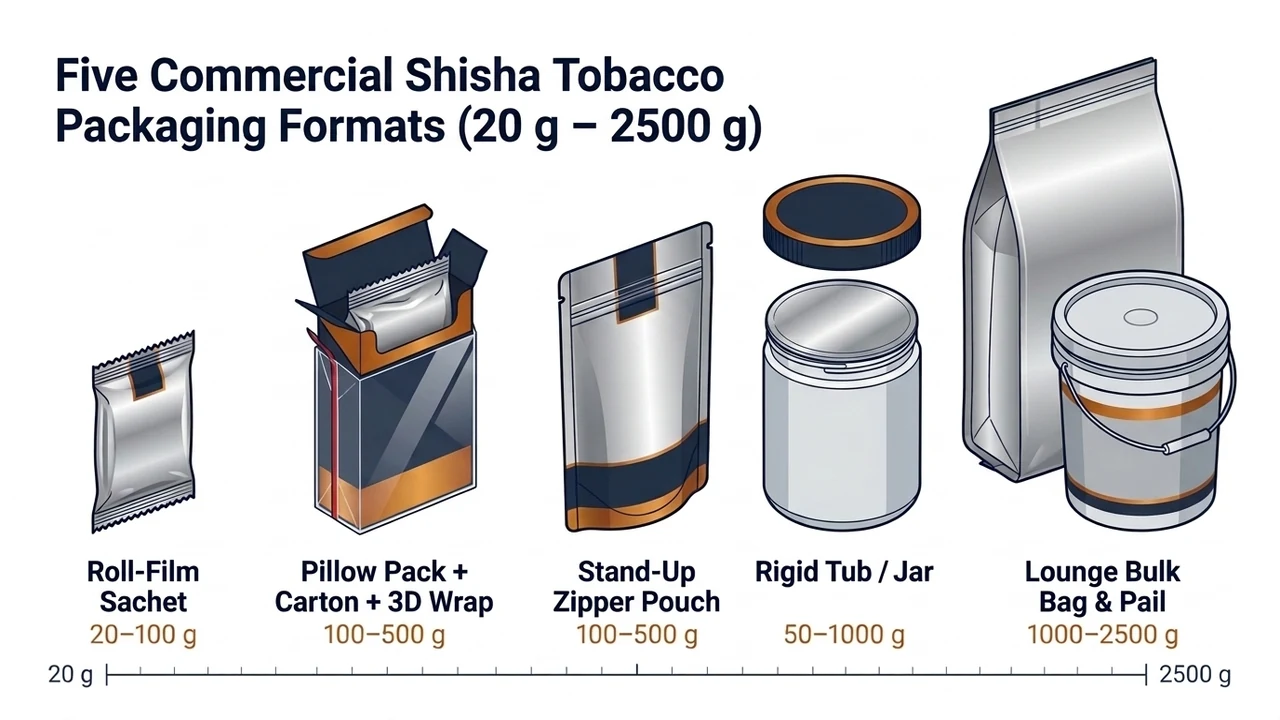
Commercial shisha packaging formats span five categories from 20 g to 2500 g: vertical roll-film sachets (20–100 g), horizontal inner pillow blocks in folding cartons with 3D overwrap (100–500 g), pre-made stand-up zipper pouches (100–500 g), induction-sealed rigid tubs (50–1000 g), and hookah lounge bulk packs (1000–2500 g). Weight window, syrup barrier, and warning-panel rules determine the right choice.
Every wet hookah tobacco format pairs with a distinct dosing and sealing architecture across our shisha packing machine lineup. Matching portion weight, molasses retention, and retail presentation before ordering prevents film-width mismatches, leaking top seams, and downstream cartoner jams.
What Are the Five Commercial Shisha Packaging Formats and Matching Machines?
The five commercial shisha packaging formats divide cleanly by gram window: LV-320SY Vertical VFFS runs 20–100 g roll-film sachets, LV-350SY Horizontal Flow and Pre-Made Pouch machines cover 100–500 g retail formats, 8-station Straight-Line or 5-station Corner-Type lines handle boxed packs, and LV-SY weighers or the 7-station tub line handle 50–2500 g bulk and rigid packs.
Within LINEVO’s 350-series range for 100–500 g shisha portions, LV-350SY is engineered in two distinct architectures: the LV-350SY Horizontal High-Speed Flow Wrapper (50–120 bags/min, 1417.5 × 750 × 1290 mm, 200 kg) for roll-film inner pillow blocks and the LV-350SY Pre-Made Pouch Machine (10–20 bags/min, 4799 × 779 × 1450 mm, 450 kg) for stand-up and zipper pouches. Buyers comparing equipment proposals should specify both the model code and architecture.
| Commercial Shisha Format | Weight Window | Barrier & Closure Structure | Matching LINEVO Equipment | Rated Speed & Footprint Envelope | Power & Machine Weight |
|---|---|---|---|---|---|
| Small roll-film sachet | 20–100 g | Roll-stock BOPP/CPP or PET/AL/PE pillow sachet | LV-320SY Vertical VFFS Machine | 10–25 bags/min; bag L 80–240 × W 50–150 mm; base frame 1185 × 935 × 1245 mm | 220V, 50Hz, 3.2 kVA; 450 kg |
| Inner pillow block for carton | 100–500 g | Compact roll-film pillow pack up to 350 mm film width | LV-350SY Horizontal Flow Wrapper | 50–120 bags/min; 80 L hopper; 1417.5 × 750 × 1290 mm | 220V, 50/60Hz, 2.4 kW; 200 kg |
| Boxed inner pack + 3D overwrap | 100–500 g (inner block) | Inner pillow pack + folding carton + 3D BOPP overwrap with tear tape | 8-Station Straight-Line or 5-Station Corner-Type Line | Extruder, pillow wrapper, checkweigher, boxing, coding, and 3D overwrap | Synchronized line power per station layout |
| Stand-up or flat zipper pouch | 100–500 g | Pre-formed PET/AL/PE pouch up to 350 mm width with zipper | LV-350SY Pre-Made Pouch Machine | 10–20 bags/min; 4799 × 779 × 1450 mm | 220V, 50/60Hz, 2.4 kW; 450 kg |
| Rigid tub or jar with foil seal | 50–1000 g | PE, PET, or heat-resistant PP tub + aluminum induction foil + screw cap | 7-Station Hookah Bottle & Tub Line or LV-SY Single | 7 automated stations (unscrambler through sorting) or LV-SY Single 1307 × 872 × 1614 mm | LV-SY Single: 220V, 50/60Hz, 1.5 kW; 250 kg |
| Hookah lounge bulk bag or pail | 1000–2500 g | Heavy bulk pouch or lidded lounge bucket | LV-SY Double Semi-Automatic Weigher | Customizable 1000–2500 g dual-lane frame; 2328 × 844 × 1614 mm | 220V, 50/60Hz dual-lane; 500 kg |
How Do You Match Shisha Weights From 20 g to 2500 g to Equipment?
Match each target SKU gram weight to the narrowest mechanical platform that covers your distribution channel: 20–100 g sachets run on LV-320SY Vertical VFFS, 100–500 g retail cartons and stand-up pouches split across the two LV-350SY platforms, and 50–2500 g flexible tubs or lounge bulk packs route to LV-SY Single and Double weighers.
No single dosing head cleanly covers both a 20 g single-session sachet and a 2500 g hookah lounge bucket. Narrow vertical forming tubes limit sticky-tobacco drop speed at higher gram weights, whereas wide horizontal extrusion hoppers and dual-lane bulk weighers overshoot small convenience portions.
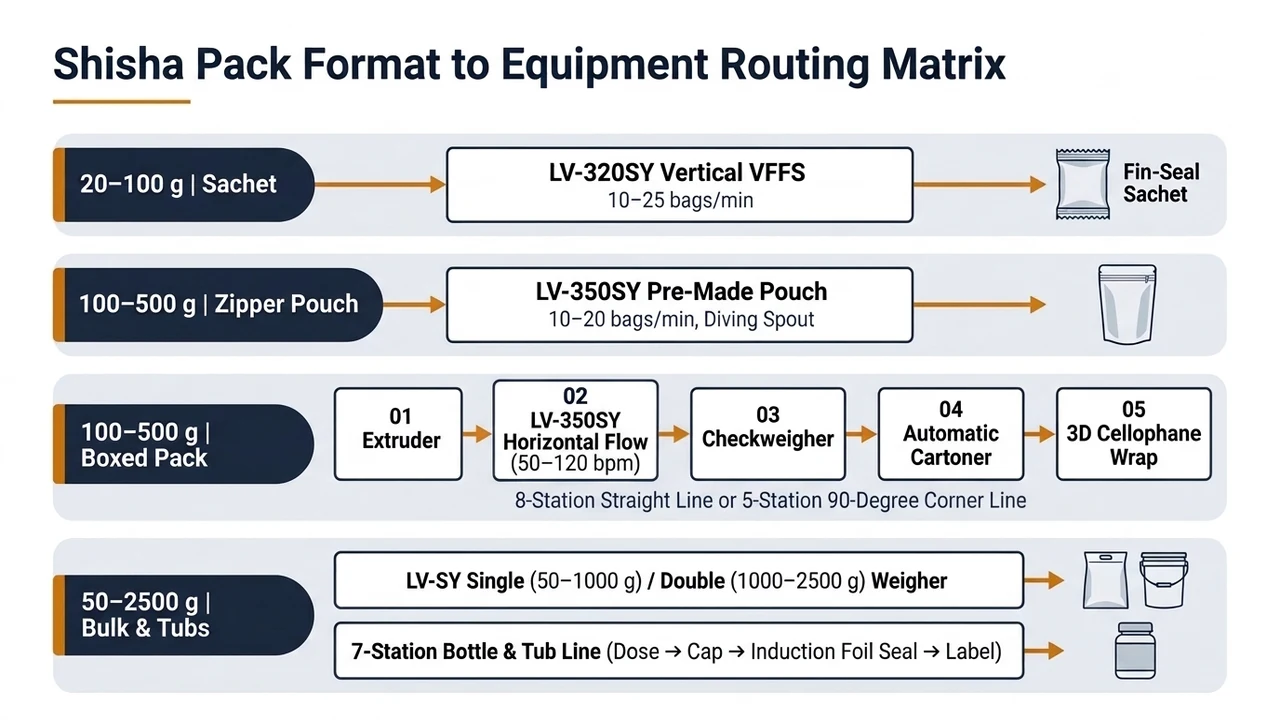
| Target SKU Weight | Common Retail or Lounge Presentation | Recommended Machine or Line | Process Envelope & Key Engineering Advantage |
|---|---|---|---|
| 20 g single-session sachet | Roll-film pillow sachet | LV-320SY Vertical VFFS | 20–100 g window; bag L 80–240 × W 50–150 mm; 10–25 bags/min |
| 50 g convenience pack | Roll-film sachet or weighed tub portion | LV-320SY Vertical VFFS or LV-SY Single | LV-320SY automates 20–100 g sachets; LV-SY Single covers 50–1000 g multi-flavor runs |
| 100 g standard retail SKU | Boxed inner pillow block or stand-up zipper pouch | LV-350SY Horizontal (50–120 bags/min) or LV-350SY Pre-Made Pouch (10–20 bags/min) | Entry threshold of the 100–500 g LV-350SY platform across roll-film and premade pouches |
| 200 g and 250 g core retail SKU | Stand-up zipper pouch, boxed inner block, or rigid tub | LV-350SY Pre-Made Pouch, 8-Station or 5-Station Line, or 7-Station Tub Line | Diving spout shields zipper tracks; flat extruded blocks slide into cartons cleanly |
| 500 g enthusiast retail pack | Large zipper pouch, heavy boxed block, or screw-cap tub | LV-350SY Platform (100–500 g) or LV-SY Single (50–1000 g) | Upper limit of LV-350SY bag wrappers and mid-range of LV-SY Single |
| 1000 g to 2500 g lounge bulk | Heavy master pouch or lidded bulk pail | LV-SY Single (50–1000 g) or LV-SY Double (1000–2500 g) | Dual-lane LV-SY Double (2328 × 844 × 1614 mm, 500 kg) meters heavy 1000–2500 g batches |
Why Do Retail Shisha Brands Pair an Inner Pillow Pack, Carton, and 3D Overwrap?
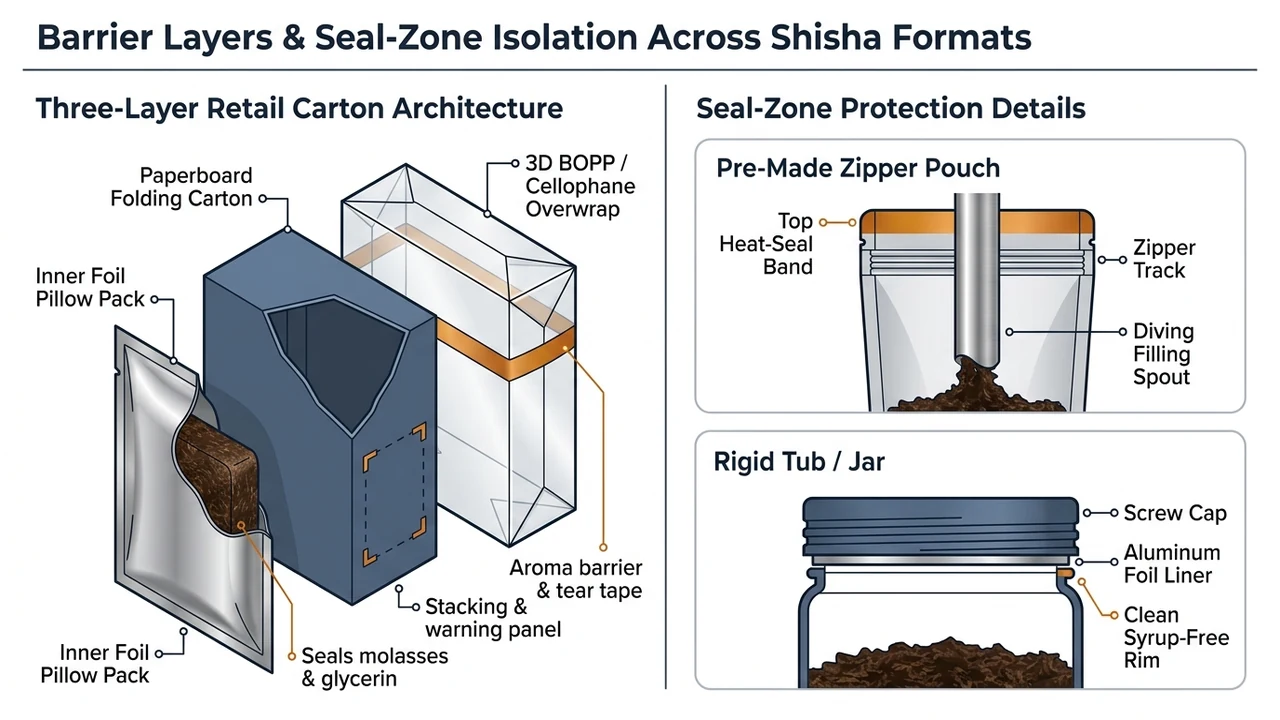
High-volume retail shisha brands stack three protective layers—a heat-sealed inner pillow pack, a rigid folding carton, and an outer 3D biaxially oriented polypropylene (BOPP) overwrap—to isolate sticky molasses internally, provide flat principal display panels for mandatory health warnings, and add a tamper-indicating outer barrier with tear tape.
Three-Layer Moisture and Mechanical Protection
In an automated shisha tobacco packaging line, each packaging layer solves a distinct physical hazard. First, the LV-350SY Horizontal Flow Wrapper draws wet tobacco from its 80 L hopper and wraps cohesive 100–500 g extruded blocks in roll film up to 350 mm wide at 50–120 bags/min, using stable temperature control and serrated or striated crimpers on BOPP/CPP or PET/AL/PE films to squeeze out minor glycerine oil films. Forming a flat, compact inner pillow block keeps syrup contained and prevents bag jams inside the downstream boxing machine.
Second, on the 8-station Straight-Line layout, Station 03 Checkweigher inspects every inner pillow pack immediately after wrapping so off-weight portions are rejected before wasting a printed folding carton or overwrap film, followed by Station 05 Weight Sorting after boxing. Third, as documented in Wikipedia’s overview of overwrap packaging, plastic films—usually polyethylene or polypropylene—applied over a secondary package help prevent pilferage or premature opening, provide a tamper-indicating seal, and combine two or more smaller packages into a multi-pack.
Biaxially oriented polypropylene (BOPP) is extruded and stretched in both the machine direction and across the machine direction, making it crystal clear for retail overwrapping and slit from large master rolls into smaller rolls sized for packaging machines. Station 07 on the Straight-Line layout (and Station 05 on the 5-station Corner-Type layout) wraps each carton in clear 3D BOPP/cellophane film with envelope-folded corners and tear-off tape, while Station 08 on the Straight-Line collates 5 or 10 cartons into master bundles.
Labeling Panel Area and Tamper-Evident Standards
Beyond mechanical protection, folding cartons and primary retail packs must satisfy strict construction and labeling rules in regulated markets. Under 27 CFR 40.211, manufacturers removing tobacco products subject to U.S. federal excise tax must put them in packages constructed to securely contain the products and maintain all required marks and notices.
For covered tobacco products manufactured, packaged, or imported for U.S. sale or distribution, 21 CFR Part 1143 sets exact panel geometry constraints that directly affect format choice:
- Panel coverage and visibility under wrap (21 CFR 1143.3): The required nicotine warning statement must appear directly on the package, remain clearly visible underneath any cellophane or other clear wrapping, and occupy at least 30 percent of each of the two principal display panels.
- Typography and contrast (21 CFR 1143.3): Warning text must use at least 12-point Helvetica bold, Arial bold, or other sans-serif font in black text on a white background or white text on a black background.
- No removable-wrapper warnings (21 CFR 1143.9): Required warnings must be indelibly printed on or permanently affixed to the package and must not be placed on a label affixed to a clear outer wrapper that is likely to be removed to access the product.
- Geographic scope (21 CFR 1143.11): Part 1143 does not apply to tobacco products that are not manufactured, packaged, or imported for sale or distribution within the United States.
For tamper-evident design benchmarks, 21 CFR 211.132 defines a tamper-evident package as one having one or more indicators or barriers to entry that provide visible evidence if breached or missing—operating either on an immediate container and closure system or on a secondary carton system—and remaining intact under reasonable handling during manufacture, distribution, and retail display.
| Format Architecture | Molasses Containment Layer | Tamper-Evident Barrier | Labeling & Warning Panel Surface | Multi-Pack Bundling Option |
|---|---|---|---|---|
| Vertical VFFS sachet (20–100 g) | Fin-seal BOPP/CPP or PET/AL/PE film | Heat-sealed primary sachet seams | Flat front and back film faces | Manual or outer display box |
| Inner pillow + carton + 3D wrap (100–500 g) | Sealed inner roll-film pillow pack | Outer 3D BOPP overwrap with tear tape | Rigid flat carton faces visible beneath clear BOPP | Station 08 collates 5 or 10 cartons into master bundles |
| Stand-up zipper pouch (100–500 g) | Multi-layer PET/AL/PE foil laminate | Heat-sealed top band above tear notch and zipper | Wide standing front and back pouch panels | Manual or shipper case packing |
| Rigid tub or jar (50–1000 g) | PE, PET, or heat-resistant PP body | Welded aluminum induction foil inner seal under screw cap | Wrap-around side label and lid | Case packing from the bottle sorting turntable |
How Do Pre-Made Zipper Pouches Compare With Rigid Tubs for Wet Shisha Molasses?
Pre-made stand-up zipper pouches deliver aluminum-foil aroma conservation, clean outer packs, and consumer reclosability across 100 g, 200 g, 250 g, and 500 g retail SKUs using diving-spout filling on LV-350SY machines, whereas PE, PET, or polypropylene tubs provide rigid scoopability sealed by Station 05 aluminum induction foil liners on the 7-station line.
Diving-Spout Isolation and Laminate Sealing in Zipper Pouches
Brands choosing pre-made stand-up zipper pouches eliminate the outer folding carton while keeping flexible barrier protection between smoking sessions. Because wet molasses drips across a zipper track or seal seam ruin closures, the LV-350SY Pre-Made Pouch Machine extends a shielded diving filling spout below both the zipper track and top heat-seal band to discharge metered 100–500 g portions cleanly.
Thick aluminum-foil barrier laminates such as PET/AL/PE retain heat longer than thin mono-films. Combining a primary heat-seal bar with a secondary seal and cooling station prevents wrinkles and micro-channels caused by glycerine vapor. Compare unit workflows and speed tradeoffs in our premade pouch vs. roll-film shisha guide, and check seal diagnostics in our shisha pouch sealing troubleshooting guide.
Heat-Resistant Polypropylene Tubs and Induction Foil Rim Seals
Rigid tubs and wide-mouth jars let hookah lounges and home users remix settled molasses syrup directly inside the container before packing a bowl. As noted in Wikipedia’s polypropylene materials reference, polypropylene tubs are heat-resistant and widely sealed with aluminum foil.
On LINEVO’s automated Hookah Bottle and Tub Filling Line, rigid containers pass sequentially through seven integrated stations: bottle unscrambler, feeding and rotary indexing, dosing and filling, screw capping, Station 05 aluminum foil induction sealing (matched to PE, PET, or PP liner material and rim diameter to prevent syrup leakage), round bottle labeling, and a bottle sorting turntable. Keeping tobacco strands completely off the container rim before capping is essential for a leak-free induction bond; see our induction foil seal guide for liner anatomy and rim inspection criteria.
How Should Multi-SKU Plants Route Formats and Verify Performance at FAT?
Multi-SKU shisha plants separate high-speed single-format retail lines from fast-washdown multi-flavor stations, then lock machine acceptance to Factory Acceptance Testing (FAT) using 200–500 sample pouches per SKU, 20–30 consecutive weighments at minimum and maximum gram targets, and clean-rim checks on rigid tubs.
Worked Multi-SKU Format Routing Example
Consider a producer running three active commercial formats across a diverse flavor catalog—a common setup among craft brands managing 10 to 30 distinct flavors alongside flagship retail SKUs:
- Flagship 250 g boxed retail SKU (high volume): Route to an extruder paired with the LV-350SY Horizontal Flow Wrapper (100–500 g, 50–120 bags/min, 80 L hopper) inside an 8-station Straight-Line layout. Station 03 Checkweigher catches off-weight inner packs before they consume a folding carton, Station 07 applies individual 3D BOPP overwrap with tear tape, and Station 08 collates 5 or 10 cartons into master bundles. If floor length is constrained and master bundling is unnecessary, substitute the 5-station 90-degree Corner-Type layout.
- Convenience 50 g roll-film sachet SKU: Route to a dedicated LV-320SY Vertical VFFS Machine (20–100 g, 10–25 bags/min, bag L 80–240 × W 50–150 mm) rather than attempting to under-fill a 100–500 g horizontal wrapper.
- 1000 g hookah lounge tubs and 10 to 30 rotating craft flavors: Route frequent small-to-medium flavor batches to an open-access LV-SY Single semi-automatic weigher (50–1000 g, 1307 × 872 × 1614 mm, 250 kg, 1.5 kW)—or LV-SY Double (1000–2500 g, 500 kg) for bulk pails—so operators can wash down contact chutes rapidly between mint, fruit, and spiced runs without stripping an enclosed high-speed line.
For full selection criteria across syrup viscosity and factory layout, review how to choose a shisha packing machine.
Concrete Format & FAT Verification Checklist
Before approving equipment shipment, bind your format specification to measurable sample testing and FAT verification criteria:
| Format Track | Pre-Trial Sample Input | FAT Verification Checkpoint | Acceptance Target |
|---|---|---|---|
| Vertical VFFS sachet (LV-320SY) | Roll-stock BOPP/CPP or PET/AL/PE film and representative wet tobacco | Bag dimensions within L 80–240 × W 50–150 mm and serrated crimper seal check | 10–25 bags/min on 20–100 g portions with clean cross seals |
| Horizontal pillow + carton line (LV-350SY + 8/5-station) | Roll film up to 350 mm width, folding cartons, and 3D BOPP overwrap roll | Flat extruded block insertion at cartoner, Station 03 reject trigger, and 3D wrap fold | 50–120 bags/min primary wrap envelope with jam-free cartoning |
| Pre-made zipper pouch (LV-350SY Pre-Made) | 200–500 physical sample pouches per SKU plus representative wet tobacco | Diving-spout clearance below zipper track and two-stage heat seal plus cooling | 10–20 bags/min across 100–500 g with zero syrup on zipper or top seam |
| Semi-automatic weigher (LV-SY Single / Double) | Representative sticky tobacco across minimum and maximum target weights | 20–30 consecutive weighments at min/max targets (50 g / 1000 g or 1000 g / 2500 g) | Documented mean weight and standard deviation at both weight limits |
| Rigid tub or jar line (7-Station Bottle & Tub Line) | Target PE, PET, or PP tubs, screw caps, and matched aluminum induction foil liners | Pre-capping rim cleanliness check and Station 05 induction foil bond check | Zero tobacco strands on container rim and leak-free induction weld |
Frequently Asked Questions
What are the five commercial shisha packaging formats?
Commercial shisha tobacco is packaged in five primary formats across a 20 g to 2500 g range: 20–100 g vertical roll-film sachets, 100–500 g horizontal inner pillow packs in folding cartons with 3D overwrap, 100–500 g pre-made stand-up zipper pouches, 50–1000 g rigid plastic tubs and jars with aluminum induction foil seals, and 1000–2500 g hookah lounge bulk pouches and pails.
Can one shisha packing machine run both 50 g sachets and 1000 g lounge tubs?
No single dosing and wrapping head spans 20 g sachets through 2500 g bulk containers cleanly. Plants route 20–100 g sachets to LV-320SY Vertical VFFS, 100–500 g pouches or inner pillow blocks to LV-350SY Pre-Made Pouch or Horizontal Flow platforms, and 50–1000 g or 1000–2500 g tubs and bulk packs to LV-SY Single or Double weighers.
Why are shisha cartons wrapped in 3D BOPP film instead of printing warnings on the outer film?
Crystal-clear BOPP overwrap helps prevent pilferage or premature opening, provides a tamper-indicating seal with tear tape, and groups 5 or 10 cartons into master bundles. For U.S.-distributed covered tobacco products, 21 CFR 1143.3 and 21 CFR 1143.9 require warning statements to be indelibly printed or permanently affixed directly on the package—visible underneath clear wrapping across at least 30 percent of each principal display panel—and prohibit placing warnings only on a removable clear outer wrapper.
What is the difference between the LV-350SY Horizontal Flow Wrapper and the LV-350SY Pre-Made Pouch Machine?
Both 350-series architectures serve 100–500 g shisha portions up to 350 mm width on 220V, 50/60Hz, 2.4 kW power, but their mechanics and speeds differ sharply. The LV-350SY Horizontal Flow Wrapper (1417.5 × 750 × 1290 mm, 200 kg, 80 L hopper) wraps roll-film inner pillow blocks at 50–120 bags/min for cartoning, while the LV-350SY Pre-Made Pouch Machine (4799 × 779 × 1450 mm, 450 kg) fills pre-formed stand-up and zipper pouches at 10–20 bags/min through a diving spout.
When should a shisha brand choose an 8-station Straight-Line vs. a 5-station Corner-Type packaging line?
Choose the 8-station Straight-Line layout when you have linear floor length and want dedicated Station 03 pre-carton checkweighing (rejecting off-weight bags before wasting cartons), Station 05 post-carton weight sorting, and Station 08 master-bundle 3D overwrapping for 5 or 10 cartons. Choose the 5-station 90-degree Corner-Type layout when workshop length is shorter and you only need extrusion, pillow wrapping, boxing, inkjet coding, and single-carton 3D overwrapping.
Sources
- eCFR — 21 CFR Part 1143 (Minimum Required Warning Statements for Tobacco Products)
- eCFR — 27 CFR 40.211 (Tobacco Product Package Construction and Marking Requirements)
- eCFR — 21 CFR 211.132 (Tamper-Evident Packaging Requirements Benchmark)
- Wikipedia — Overwrap (Film Overwrapping Materials, Multi-Packing, and Tamper-Indicating Functions)
- Wikipedia — Polypropylene (BOPP Biaxially Oriented Film and Heat-Resistant Polypropylene Tubs)
Configure Your Shisha Packaging Line with LINEVO Engineers
Send your shisha tobacco pack format, target gram weight, and required speed on WhatsApp to receive technical drawings, trial videos, and an itemized factory quotation, or check our RFQ preparation checklist.
Get Quote via WhatsAppBrowse all Shisha Packaging Guides